Bagging machines for grain, fertiliser, pellets, coal and powders. 5–50 kg bags, ±50–200 g accuracy. Let us help you choose the right model.
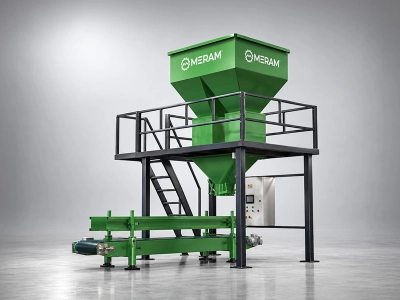
M-DF1Double Gate Bagging Machine
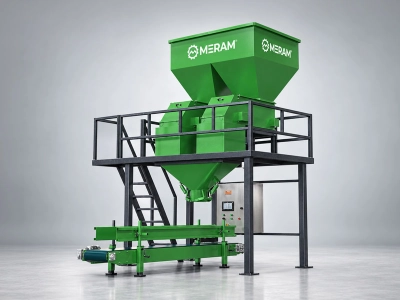
M-DB1Double Belt Bagging Machine
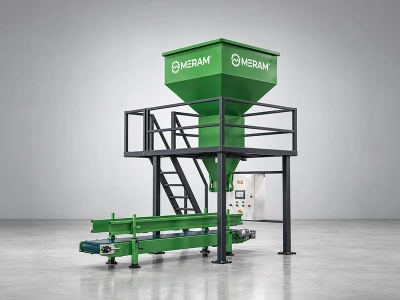
M-SF1Single Gate Bagging Machine
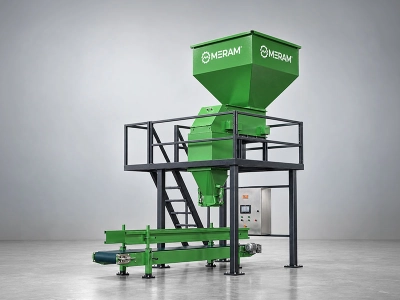
M-SB1Single Belt Bagging Machine
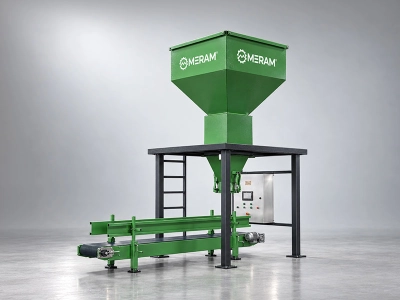
M-SF2Economical Single Gate Bagging Machine
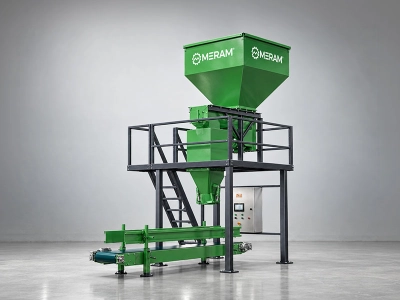
M-AF1Auger Bagging Machine
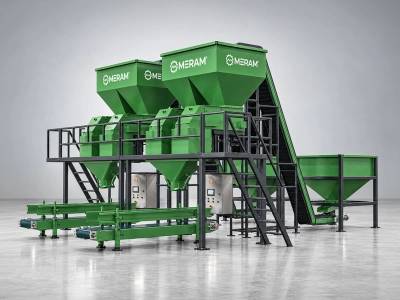
M-DB2-2LTwo-Station Double Belt Bagging Machine ProBBF big bag filling machine for powders and granules: 500–2000 kg bags, 15–30 bags an hour, fed by gravity, belt or auger.
All Big Bag Filling Machines modelsWeigh-based liquid filling machine for jerrycans, tins, pails and drums: two-stage fast and slow filling, net or gross mode, Ex-proof option.
All Liquid Filling Machines modelsTruck scales for surface or pit installation, with steel-reinforced concrete, I-beam or V-beam steel decks. 6–22 m long, 40–100 t capacity.
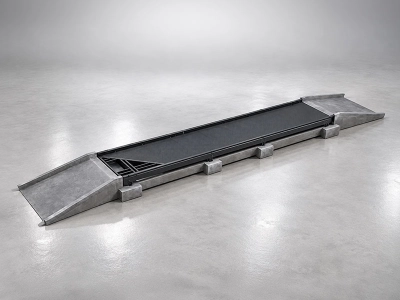
WB-X800FI-Beam Steel Platform Truck Scale
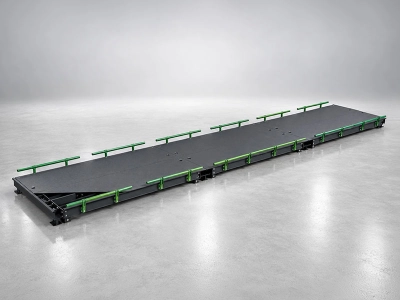
WB-X600V-Beam Bridge Type Truck Scale
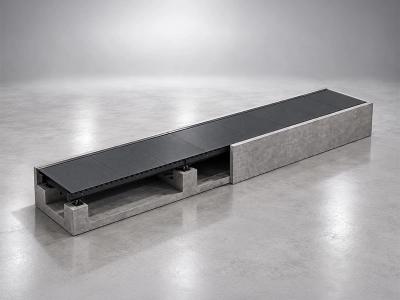
WB-X800PI-Beam Steel Pit Type Truck Scale
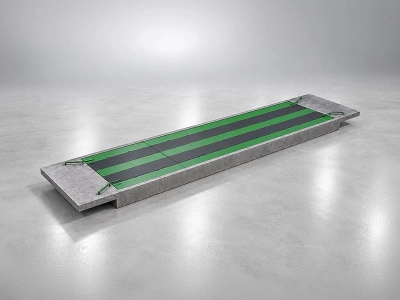
WB-X400PSteel-Reinforced Pit Type Truck Scale
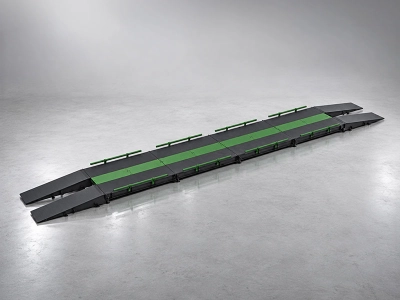
WB-X400FSteel-Reinforced Concrete Truck ScaleCheckweighers that weigh every pack in motion and reject under- and overweight packs: CW, and MCW for compact lines. Rejection, reporting, retrofit.
All Checkweighers modelsHeavy-duty floor scales: CP, TP, U-type pallet scale, MB modular, steel bar and marble scales. Four OIML R60 C4 load cells, sized to the load.
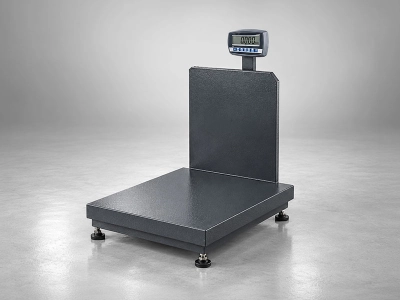
All Heavy Duty Scales modelsBS single load cell platform scale: 30 kg–1.5 t, double-chassis electronic construction and dual-range weighing for bench and packing use.
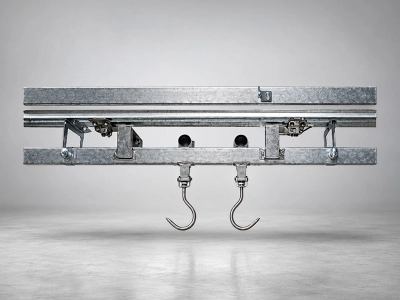
All Bench Scales modelsMonorail scales for abattoirs and meat plants: carcasses are weighed on the rail. Fitted to your existing line, stainless or galvanised.
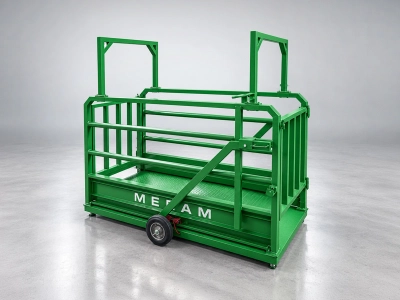
All Monorail Scales modelsLivestock scales for cattle, sheep, goats and sacrifice shares: the 80 mm low-profile BBH, gated KBH and a 7-point share scale.
All Livestock Scales modelsBK belt weigher for weighing bulk material on the conveyor without stopping the line: 800–2000 mm belts, flows up to 6000 t/h.
All Belt Weighers modelsFarms, feedlots and grain businesses.
Weighbridge yards, warehouses and dispatch.
Packing, filling and end-of-line checking.
Bulk material and vehicle weighing.
Liquid and powder filling.
Vehicle and platform weighing.
Surface and pit-mounted weighbridges for trucks and tractors.
Cattle and small livestock; low platforms for the farm.
Floor scales, pallet scales and single-cell platform scales.
Continuous flow and totalised weight on the belt.
Bag, big bag and liquid filling; automatic weighing lines.
Weighs packed products in line and rejects under- and overweight.
Products
Also known as a conveyor scale, a belt weigher is a measuring system that weighs bulk material on a conveyor while the line keeps running. Load cells supporting the idlers in the weighing zone measure the weight of material on the belt, and a separate sensor measures belt speed. Combining the two gives the current flow rate in tonnes per hour; adding that flow up over time gives the total quantity that has passed along the conveyor.
Sending a lorry to the weighbridge or estimating the volume of a stockpile tells you how much material has moved, but late and indirectly. A conveyor belt scale shows production, loading and stock movement while the material is moving, not at the end of the shift. BK belt weighers are made for belts 800–2000 mm wide and flows of up to 6000 tonnes per hour, and handles powders, granules and lumpy material.
The same measurement can serve several purposes. The needs we meet most often are these. In short:
| Feature | BK |
|---|---|
| Belt width | 800–2000 mm |
| Flow rate | Up to 6000 t/h |
| Material | Powders, granules, lumps |
| Mounting | On an existing conveyor, between the carrying idlers |
| Speed measurement | Belt speed sensor |
| Output | Instantaneous flow (t/h) and totalised weight |
The principle is a simple multiplication. Suppose there is on average 50 kg of material on each metre of belt in the weighing zone, and the belt moves at 2 metres per second. Then 100 kg passes every second, which is 360 tonnes per hour. The belt weigher repeats this calculation continuously; whenever load or speed changes, the flow value updates and the total keeps building without interruption.
BK is designed to be added to an existing conveyor. The weighing unit sits between the carrying idlers, the speed sensor reads belt speed and the indicator combines the two to show flow and total. No major change to the conveyor itself is needed; belt width, conveyor incline and the nature of the material are reviewed with you before we quote.
A belt weigher is a calculation that combines two measurements without pause. The weighing bridge measures the load on the section of belt passing over it, and this value is divided by the length of the weighing zone to give load per metre. The speed sensor reports how far the belt has travelled. Load per metre multiplied by belt speed gives the instantaneous flow rate; summing that rate over very short intervals, in other words integrating it, gives the total material that has passed along the conveyor.
This has a practical consequence: errors can come from two separate sources. Even with perfect load measurement, a wrong speed reading makes the total wrong. Even with the right speed, if the bridge does not sense the full load carried by the belt, the result drifts. So when assessing a belt weigher, look not only at the load cells but also at speed measurement and at how well the bridge fits the conveyor.
The weighing bridge is the frame that seats one or more carrying idler stations of the conveyor on load cells. The idlers on the bridge must sit at the same height and in the same line as their neighbours. A difference of just a few millimetres makes the belt press harder on the bridge, or lift off it, and the measured load moves away from the real one. For this reason the idler stations just before and after the bridge also count as part of the measuring system and are aligned with it during installation.
The spacing of the idler stations and the number of stations the bridge covers set the length of the weighing zone. A longer zone averages out material that is unevenly spread on the belt. A shorter zone responds faster but gives a jumpier result when the load fluctuates. Which suits you depends on how steady your flow is.
The speed sensor is usually coupled to a pulley that turns with the belt, or to a wheel running against the underside of the belt, and reports the distance travelled as pulses. It must read the belt without slipping: a slipping wheel or a worn pulley face spoils the total however good the load measurement is. Even on conveyors assumed to run at constant speed, speed varies somewhat with load and tension, which is why measuring the actual speed gives more reliable results. On conveyors whose speed is set by a variable-frequency drive the measurement is indispensable; a calculation made without it produces a wrong total every time the drive speed changes.
The two systems do not replace each other; they complement each other. A weighbridge gives the total of a shipment by weighing the vehicle in and out; it produces one result per vehicle and needs no conveyor. A belt weigher produces data continuously while material is moving, showing how much flowed at what time, where the flow slowed and how it fluctuated during the shift. Where material moves around the site by conveyor and process management needs live information, the belt weigher comes first; where an exact weight per vehicle is needed for dispatch and invoicing, the weighbridge does. Many mines and aggregate plants use both: the belt weigher tracks production, the weighbridge tracks sales.
Belt weighers are used to monitor tonnage wherever bulk material is carried continuously by conveyor:
A belt weigher’s performance depends as much on the condition of the conveyor as on the device itself. Before quoting, we look at these together:
1. Flow and belt width. Hourly tonnage and belt width set the size of the weighing unit. The BK series is configured for 800–2000 mm belts and flows of up to 6000 t/h; both the lowest and the highest flow need to be known.
2. Belt speed and incline. Load per metre of belt is the flow divided by the speed. A flow of 360 t/h on a belt moving at 2 metres per second means 50 kg per metre; at 1 metre per second the same flow puts 100 kg on each metre. On steeper inclines, the tendency of material to slide back is also taken into account.
3. Nature of the material. Powders, granules and lumps spread differently on the belt. Sticky or damp material clings to the belt and shifts the zero point, which makes belt cleaners and frequent zero checks more important.
4. Mounting section. The unit needs a level or constant-incline stretch with steady tension, well clear of the feed point and any curves. On a short conveyor, where that section will be is agreed at the quotation stage.
5. Purpose of measurement. Process monitoring and trade create different expectations. For trade use, legal metrology rules apply.
6. Environment. Outdoors, dust, rain and temperature swings; indoors, vibration and nearby machinery are taken into account.
Calibrating a belt weigher is not a one-off job but a maintenance routine. Three steps complement each other:
Zeroing. The empty belt is run for several complete revolutions and the average reading over that period is taken as zero. Because the belt does not weigh the same at every point, the average of full revolutions is used rather than a single instant reading. Zero should be taken again after a belt change or splice, or whenever material is found sticking to the belt.
Weight or chain test. A known load is hung on the weighing zone, or a calibration chain of known weight is laid on the belt, and the belt is run for a set time. The total shown is compared with the value expected from the load multiplied by speed and time. It is quick and suits frequent checks on the consistency of the bridge and speed measurement.
Material test. A quantity of material already weighed on a separate scale is run over the belt, or the material that has passed is weighed afterwards. The result is compared with the total recorded by the belt weigher. Because it uses real material under real operating conditions, it is the most meaningful check. For example, if the belt weigher shows 20.3 tonnes for a 20-tonne test batch, the deviation is 1.5% and the calibration factor is corrected accordingly.
Most of these are kept under control with a written maintenance list: regular zero checks, inspection of idlers and scrapers, chain or weight tests at set intervals and material tests less often. Deciding at the outset who carries out the list, and how often, keeps the measurement trustworthy months later.
Crushing and screening plant. Belt weighers on the discharge belts show how much of each fraction is produced per shift. The effect of a crusher setting change on the product split is visible the same day, without surveying stockpiles.
Loadout belt. On a belt loading lorries or wagons, the operator watches the total on the indicator and finishes loading at the target quantity. Over- or under-loading is noticed while loading, not when the vehicle reaches the weighbridge.
Raw material feed. The quantity of raw material going to a mill or kiln is recorded per shift. Consumption is compared with output to work out losses.
Blend monitoring. When materials arriving on two separate belts are measured individually, the blend ratio can be followed in real time. With 300 t/h on the main belt and 30 t/h on the additive belt, the additive makes up about 9% of the total; if the ratio drifts from target, action can be taken without delay.
BK is matched to your conveyor, so we will need:
We reply to quotation requests within 3–4 hours.
Yes. The BK weighing unit fits between the carrying idlers of a working conveyor, while a separate sensor reads belt speed. The conveyor does not need to be rebuilt; the mounting section just has to be suitable for measurement.
Choose a section with constant tension, well clear of where material lands on the belt and of curves where the belt changes direction. The belt should run level or at a single constant angle there. A belt weigher fitted in the wrong place gives inconsistent results, however well it is calibrated.
There are two ways. In the first, a known load, meaning test weights or a calibration chain, is placed on the weighing zone. In the second, a quantity of material already weighed on a separate scale is run over the belt and compared with the total the belt weigher records. Regular zero checks on an empty belt prevent drift caused by belt wear and material sticking to the belt.
The mounting location, changes in belt tension, idler alignment, material stuck to the belt and conveyor vibration all have a direct effect. Most of these are kept under control by choosing the right location at installation and by regular zero checks.
Weighing instruments used in trade are covered by legal metrology and are subject to verification under the relevant regulations. Tell us at the quotation stage whether you will use the belt weigher for process monitoring or for sales and invoicing, so that selection and installation are planned accordingly.
Price depends mainly on belt width, flow rate, the length of the weighing zone, conveyor incline and site conditions. Whether the data only needs to be shown on the indicator or must be passed to another system also affects the quotation.
A belt weigher gives its most consistent results on belts that are loaded continuously within a reasonable part of their design range. If the belt often runs empty or carries very little material, small deviations from the belt itself account for a larger share of the total. If your flow varies considerably during the day, share the lowest and highest values at the quotation stage so that the weighing zone is chosen for that range.
Yes, on a section where the incline stays constant. On a slope, part of the load acts along the belt rather than perpendicular to the idlers; calibration takes this into account. What matters is that the incline does not change across the weighing zone and that material does not slide back on the belt.
Not sure which model fits?
Tell us the capacity, platform size and site; we will work out the right model and price together.