Applications
Wherever carcasses travel on a rail, a monorail scale makes weighing a natural step in the line:
- Red meat abattoirs: weighing cattle, sheep and goat carcasses after slaughter
- Integrated meat plants: several weighing points from slaughter to dispatch
- Municipal slaughterhouses: recording carcass weight as part of the slaughter service
- Chillers: cold carcass weight and chilling loss
- Cutting plants: recording the weight of carcasses going into cutting
- Wholesale meat trade: handing over and receiving hanging carcasses by weight
Choosing a monorail scale: the key points
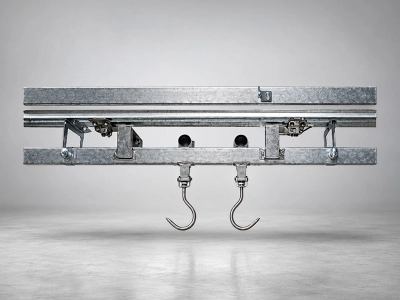
With overhead rail weighing, how well the scale fits the line matters as much as the scale itself. When we propose a scale for a line, we weigh up the following together:
1. Rail and trolley fit. The weighing section must have the same section as the existing rail and must not jolt the trolley at the joints. Otherwise the carcass jerks as it enters the section and the reading takes longer to settle.
2. Heaviest hanging load. Capacity is chosen for carcass, hook and trolley together, plus a margin. A carcass knocking into the weighing section also creates a momentary load, so the margin should not be tight.
3. Conditions and cleaning. The slaughter hall brings damp, blood and frequent washing; the chiller brings low temperatures. The frame is chosen in stainless steel or hot-dip galvanised steel to suit, and the indicator ideally sits outside the wash-down area or in a protected spot.
4. Indicator position. The operator should be able to read the value without leaving the line. Its height and angle are set during installation to suit the layout.
5. Records and traceability. If carcass weight is used for payment, chilling loss and dispatch, writing values in a book by hand invites mistakes. If recording needs are discussed from the start, the indicator is chosen to match.
6. Line speed. Weighing should not slow the line. For example, if 400 carcasses are processed in an 8-hour shift, that is 50 carcasses an hour, or 72 seconds per carcass on average. Time spent in the weighing section should be a small part of that. If throughput is to rise later, plan the weighing point for the target number of carcasses rather than today’s; otherwise the weighing point becomes the first bottleneck when the line speeds up.
Hot and cold carcass weight: working out chilling loss
A carcass weighed straight after slaughter is warm and carries moisture on its surface. During its time in the chiller its temperature falls, water evaporates from the surface and its weight drops a little. This difference is called chilling loss. For a meat business it is a direct cost: payment or sale is usually based on either the hot or the cold weight, and the difference comes out of somebody’s account.
The sum is simple. For example, if a carcass weighed at 300 kg after slaughter weighs 294 kg after chilling, the loss is (300 − 294) ÷ 300 × 100 = 2%. In a plant processing 100 carcasses a day, an average difference of 6 kg per carcass adds up to 100 × 6 = 600 kg a day. That figure alone shows why chilling loss is worth tracking: a small improvement in chilling conditions can turn into a difference measured in tonnes by the end of the month.
To track chilling loss reliably, both the hot and the cold weight of the same carcass must be recorded. This is done with two weighing points, or by passing the carcass through the same weighing section again as it leaves the chiller. Once weighings are matched to carcass numbers, losses can be compared carcass by carcass, batch by batch or chiller by chiller.
Recording, labelling and traceability
Carcass weight is the starting point for many documents in a meat business: payment to the farmer, the invoice for slaughter services, dispatch notes and internal stock records are all derived from it. Reading the value off the indicator and writing it on paper by hand leaves the door open to reading and writing mistakes on a busy slaughter day.
In an orderly recording system, each weighing is stored with the carcass number, date and time, species and, where needed, the farmer or batch. Depending on the plant’s needs, the value can be printed on a label attached to the carcass or passed to the business’s records. The method chosen directly affects the choice of indicator, so discussing recording needs at the quotation stage avoids changes after installation.
The traceability rule is simple: if asked later, the records should show which animal a carcass came from, when it was slaughtered and at what weight it went to which customer. Weighing is the measured link in that chain.
Differences between cattle and sheep lines
Cattle and sheep slaughter lines follow the same rail principle but make different demands on weighing. Cattle carcasses are usually split down the middle and hung as sides; the load on a single hanger is heavy, the carcass is long and its swing dies away more slowly. On these lines, fixing the weighing section to a strong support and keeping the entry as smooth as possible come first.
On sheep and goat lines, individual loads are light but numerous. Hangers are spaced more closely and the line runs faster. What matters here is that the weighing section is short enough never to carry two hangers at once, and that the indicator captures a stable value quickly. If both species run on the same line, capacity is set by the cattle and section length by the spacing of the sheep hangers; where the two requirements conflict, separate weighing points are the sounder solution.
On lines where a carcass hangs from more than one hook, the weighing section must be arranged to carry all of them together. Otherwise part of the load rests on rail outside the weighing section and the reading comes out short.
Hygiene and wash-down
A slaughter hall is a place where equipment in direct contact with food is cleaned often. With a monorail scale, hygiene starts with the choice of material and continues with cleaning habits:
- Material: the frame is chosen in stainless steel or hot-dip galvanised steel to suit the plant’s conditions and cleaning routine
- Surfaces that do not trap dirt: recesses and gaps around the weighing section where blood and fat can collect must not be skipped during cleaning
- Electronics: the indicator and cable connections are placed away from washing water or in a protected position, and pressure jets are never aimed at them
- Cleaning chemicals: cleaning and disinfection products are chosen to be compatible with the frame material
The hygiene rules and cleaning programme a plant must follow vary from business to business; the position and material of the scale are planned to fit that programme.
Measurements to take from the line before installation
Because the scale is built into the line, accurate measurement is the most important step of installation:
- Rail section: profile type and dimensions, ideally with a photo of the section
- Trolley and hook: the type of hanging gear used
- Weighing point: a straight, level stretch of rail where the carcass can hang freely
- Supporting structure: the beam or ceiling structure the rail is fixed to
- Indicator position: a spot the operator can read, away from washing water
Steps to integrate with an existing rail
Any work on a running line affects the slaughter schedule, so integration is planned to disturb the line as little as possible:
- Survey and measurement: rail section, hanger spacing, supporting structure and indicator position are established on site
- Manufacture: the weighing section is built in the workshop to those measurements and the rail profile
- Installation: the line stoppage is timed for when there is no slaughtering; the relevant piece of rail is removed and the weighing section fitted in its place
- Adjustment and trial: checks are made with loads of known weight, followed by trial weighings with real carcasses at the line’s normal pace
Maintenance and periodic checks
Maintaining a monorail scale is not complicated, but it should be regular. Because it is a part of the rail that carries load all day, mechanical checks come first:
- Rail joints: if the joints at the entry and exit of the weighing section wear or develop a step, carcasses jolt as they enter and the reading takes longer to settle
- Free movement: check that the weighing section works without touching surrounding parts; anything rubbing against it carries part of the load outside the weighing
- Fixings: bolts into the supporting structure and hanging points are inspected at intervals
- Check weighing: a check with a known load is repeated, particularly after maintenance and repairs
- Cables and indicator: look for damage to cable sheaths from washing or knocks
For an MRS proposal that fits your line, just tell us:
- The carcass type: cattle, sheep and goats, or both
- The approximate heaviest load hung on the line
- The rail profile and trolley and hook type, ideally with photos
- Where weighing will take place: after slaughter, at the chiller or at dispatch
- Whether you prefer a stainless or galvanised frame
- How weights will be recorded: by hand, on a label or passed to your business records
We reply to quotation requests within 3–4 hours.