What is a liquid filling machine?
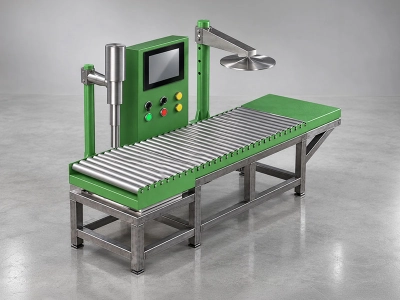
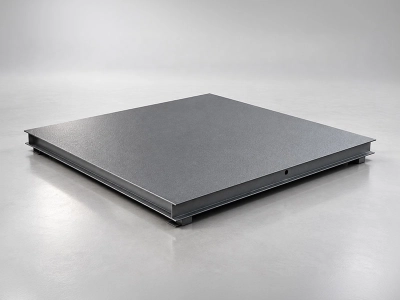
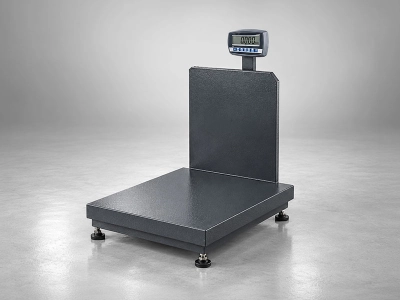
A liquid filling machine transfers a set amount of paint, chemicals or food liquids into packs such as tins, jerrycans, pails and drums. LF does this by weight rather than volume: the container stands on a weighing platform while the liquid flows in, and the filling valve closes when the weight reaches the target. That makes LF a weigh-based filler for jerrycans, tins and drums sold by the kilogram; small bottles and cosmetic or pharmaceutical packs are usually filled on different, volumetric machines.
Filling with a measuring jug or by eye causes two problems at once. First, the same litre weighs a different number of kilograms depending on temperature and density, so the weight on the label does not hold from batch to batch. Second, an operator trying to finish the last part either overfills or stops short, which means lost product and extra cleaning. Weigh filling removes the first problem because it measures kilograms directly, and two-stage filling solves the second.
Which filling set-up suits my product?
LF is a single model, configured differently to suit the product and the container. In short:
- Paints, varnishes and chemicals sold by the kilogram: net filling, with the container’s tare deducted
- Packs whose total shipping weight must be known: gross filling, container included
- Liquids that foam or splash: a longer slow stage
- Solvent-based products giving off flammable vapour: the Ex-proof option
- Corrosive chemicals: a filling valve in a material suited to the product
Two-stage filling: speed and accuracy together
A single-speed valve leaves two choices: fill fast and overshoot at the end, or fill slowly and give up output. LF splits filling into two stages. Most of the container fills at a high rate; as the weight nears the target the valve throttles back and the final part goes in slowly. Each container spends little time at the station, and the margin for overshooting the target shrinks.
Net and gross filling
In net filling, the empty container is weighed first and its tare deducted, so the machine counts only the liquid that goes in. Because metal tins and drums can vary slightly in weight, this mode is preferred for products labelled with a net weight. In gross filling, container and contents are filled to a combined target, which is useful when total shipping weight matters. Both modes can be selected on the same machine.
Ex-proof option: solvents and flammable products
When thinners, solvent-based paints and similar products are filled, flammable vapour builds up in the air. In such plants the electrical equipment has to be suitable for an explosive atmosphere. LF can be configured with an Ex-proof option for this. Telling us your plant’s zone classification at the quotation stage is enough for us to choose the right equipment.
By container: tins, jerrycans, pails and drums
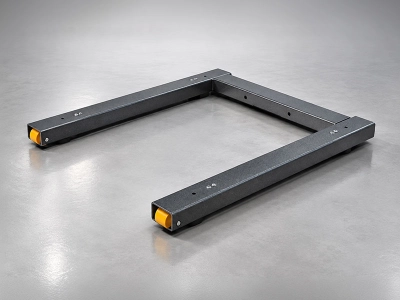
Tin filling, jerrycan filling and drum filling all rely on the same weighing principle; the differences come from the container’s opening, height and own weight. With a narrow-necked jerrycan, the question is how the spout enters it; with a wide pail, how to stop splashing; with a heavy drum, how it is brought onto the platform. These details are settled at the quotation stage from your container dimensions.
Weigh filling versus volumetric filling: where the difference starts
Volumetric fillers measure a set volume, sending the same number of litres into each container with a piston, a pump or a timed valve. For small packs, high counts and products of constant density, this is fast. But if the product is sold by the kilogram, volume is only an indirect measure: density sits between volume and weight, and density can change from batch to batch, or even within a day.
Weigh filling removes that intermediate step. The container fills while standing on the weighing platform and the machine follows the kilograms directly. The method has a cost: stable weighing needs the container to stand still on the platform and the final part to flow slowly, so on very small packs it is not as fast as a volumetric machine. Weigh filling comes into its own with tins, jerrycans, pails and drums, where weight and value per container are high and a few grams of error repeat on every container.
Viscosity, foaming and temperature
Viscosity. A thin solvent and a thick filler paint flow through the same valve opening at very different rates. With a thick product the fast stage lasts longer, and more product is “in flight” between spout and container after the valve closes. In two-stage filling, the stage changeover point and the final cut-off point are therefore set for the product: the valve closes slightly before the target and the product still falling completes it. Because viscosity also changes with temperature, a line running on the same settings in winter and summer may need its changeover points reviewed with the season.
Foaming. Detergents, some resins and emulsions foam when they fall freely into the container. The foam makes the container look full too early and then causes overflow. With foaming products, feeding the liquid below the surface from a point close to the container base and keeping the fast stage short reduce foam markedly.
Temperature. Liquids expand as they warm; the same weight of product takes up more volume when hot. In volumetric filling a temperature change turns straight into a weight error. In weigh filling the weight stays the same; even so, if product is filled hot, the headspace left in the container should allow for the product contracting as it cools.
Subsurface filling and drip control
The method where the spout is lowered into the container and the liquid is delivered below the surface is called subsurface or dip-tube filling. In general practice the spout begins close to the container base and is raised as the liquid level climbs. It reduces foaming and splashing, and with flammable products it limits the vapour that free fall would generate. With narrow-necked jerrycans, the spout diameter is chosen to suit the container opening.
Product dripping from the spout after filling soils the outside of the container and the weighing platform; with pails and tins, paint dripping onto the lid seat creates extra cleaning work. To prevent drips, the way the spout tip closes is chosen for the product’s viscosity, and the tip is given a moment to drain inside the container before it leaves the station. Which spout arrangement suits LF for your containers and product is decided at the quotation stage.
Container types and openings
- Tins: common for paints and varnishes; lidded or with a pouring opening, and being metal they vary slightly in weight
- Jerrycans: mostly narrow-necked plastic containers; the spout must enter the opening easily and the light container must not topple during filling
- Pails: wide open tops; splash control and keeping the rim clean before the lid goes on are the main concerns
- Drums: heavy and tall; usually filled through the bunghole on top, and getting the drum safely onto the platform and removing it full need their own planning
Taring and records
In net filling, each container is weighed before filling; the empty container weight is zeroed and only the liquid going in is then measured. With plastic containers of consistent weight it is generally possible to work with a fixed tare value, but with metal tins and drums weighing each container individually is safer. If fill weights need to be recorded or printed on labels, say so at the quotation stage; a printer or data connection on the indicator is planned around it. Recorded weights also help when a complaint arrives, showing what weight a given batch was filled to; with large containers, such a record puts the discussion on a documented footing.