What is a checkweigher?
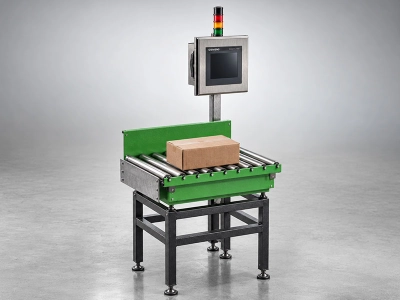
Also called a check weighing system, a checkweigher weighs every pack passing along a production line without stopping it and rejects those that fall outside the set tolerance. An automatic checkweigher measures each pack as it travels over the belt, compares the result with the target weight entered for that product and removes any pack outside the acceptance limits. Every pack or case heading to the customer is therefore weighed once more before dispatch.
Catching bad packs is only part of the job. Because the weight of every pack is recorded, the average, the spread and the drift of filling over time become visible in figures. An underweight pack means a customer complaint and an inspection risk; an overweight pack is product that never appears on an invoice. A well-installed checkweigher reduces both: it removes underweight packs and, by making overfilling visible, lets you lower the target with confidence. For each product, the number of packs weighed, accepted and found under or over the limits is reported separately.
Checkweigher or manual sample weighing?
Before moving to a checkweigher, many plants take a few packs off the line at intervals and weigh them on a bench scale. This shows roughly where filling sits, but it looks at a very small slice of the line. A simple calculation shows the gap: a line producing 60 packs a minute turns out 3,600 packs an hour. If 5 packs an hour are weighed, about 1.4 in every thousand are checked; everything else is assumed.
The second weakness of sampling is delay. If the filler starts to drift between two samples, nobody notices until the next check, and the packs produced in the meantime are already in cases. The third is record-keeping: handwritten values can be incomplete, and when a question about a batch arrives later there is no reliable data to fall back on. A checkweigher solves all three by weighing every pack. Manual weighing does not disappear entirely; it continues as a short, regular step to confirm that the checkweigher itself is working correctly.
Which checkweigher should I choose?
The first things to look at are the length of line available, the pack size and how rejected packs should leave the line. In short:
- Fully automatic weight checking and rejection on food and packaging lines: CW automatic checkweigher
- Short, compact lines with little space: MCW checkweigher
- Existing lines where a check point will be added later: measure the line first; CW if there is room, MCW if space is tight
- Rejection method: chosen independently of the model, according to pack weight, shape and line speed
Models at a glance
| Model | Purpose | Line type | Rejection |
|---|
| CW | In-line pack weight verification | Food and packaging lines | Automatic; method chosen to suit line and product |
| MCW | Weight checks on compact lines | Lines with limited space | Built to order |
CW automatic checkweigher
CW weighs packs in motion on the line and automatically rejects any pack that falls under the lower tolerance or exceeds the upper one. For each product a pack name, target weight and upper and lower tolerances are defined; when the product changes, the operator picks the matching record from the list. Because it is configurable, belt size, rejector type and reporting are set to suit the line. Installed straight after a filling or packing machine, it also brings filling drift to light early. On fast-running food and packaging lines where every pack must be verified, this is the model to consider first.
MCW checkweigher: compact lines
MCW is designed for plants where the line is short or where little room is left for a checkweigher in the existing layout. On small packing lines and at check points added later, it is a practical way to check weight without reorganising the line. Because a compact design means a shorter belt, the relationship between pack length and line speed is assessed using the calculation described below.
How does dynamic weighing work?
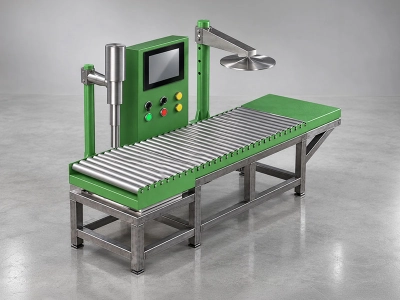
A checkweigher is a short series of conveyors inserted into the flow of the line. A typical layout has three sections, each with its own task:
- Infeed (accelerating) belt: Takes the pack from the previous conveyor and brings it up to weigh belt speed. Running the infeed slightly faster than the line opens up the gaps between packs, so only one pack at a time reaches the weigh belt.
- Weigh belt: A short, light belt mounted on one or more load cells. While the pack is on this belt the signal is read, fluctuations caused by vibration are filtered out and the weight is calculated.
- Outfeed and reject section: If the result is out of tolerance, the reject mechanism fires at the moment the pack passes it. Accepted packs carry on down the line.
Keeping the weigh belt light matters: the load cell carries not only the pack but also the belt, rollers and motor. The smaller this “dead load”, the better the same load cell can tell small differences apart on light packs.
Belt speed, pack spacing and weighing time
The decisive quantity in dynamic weighing is how long a pack sits alone and fully on the weigh belt. Three values set that time: line speed, the pack’s length in the direction of travel and the length of the weigh belt. The figures below are chosen only to show how the calculation works:
- The line delivers 60 packs a minute; each pack is 200 mm long with a 300 mm gap between packs.
- The distance from the front of one pack to the front of the next is 500 mm. With one pack passing every second, the belt must run at 0.5 m per second (30 m per minute).
- With a 400 mm weigh belt, once the pack is fully on the belt it travels 400 − 200 = 200 mm, giving a weighing window of 0.4 seconds.
- Because the belt is 400 mm and the pitch is 500 mm, there are never two packs on the belt at once.
If the same line is pushed to 120 packs a minute with the same spacing, belt speed doubles and the weighing window drops to 0.2 seconds. The shorter the window, the less time is left for filtering and the wider the spread of results. That is why line speed, pack length, belt length and expected accuracy are worked out in one calculation; changing one affects the others.
Factors that affect accuracy
Checkweigher accuracy is not expressed as a single figure but as how widely the results scatter when the same pack is passed through many times. The main factors that widen that scatter are:
- Vibration: A press, compressor, vibratory feeder or another machine on the same frame reaches the load cell directly as signal noise.
- Floor: A flexing mezzanine floor or uneven ground used by forklifts is a reference that moves during weighing. A solid, level floor matters as much as adjusting the feet.
- Air movement: An air-conditioning outlet, a fan or a frequently opened door creates a force that adds to or subtracts from the weight, especially with light packs. If needed, the weigh section is enclosed with a draught shield.
- Pack length and shape: Long packs shorten the weighing window; tall, narrow products sway or topple. In filled bottles, the liquid sloshing inside also shows up in the signal.
- Belt speed: Higher speed shortens weighing time and increases the impact as the pack transfers onto the belt.
- Temperature: Large swings in ambient temperature and heat from hot-filled products can shift the zero point. Automatic zeroing intervals are therefore set to suit conditions.
- Belt cleanliness: Product residue or dust building up on the belt changes the dead load. Regular cleaning and zeroing keep this effect in check.
Zone classification: under, accept, over
A checkweigher places every pack in a class. In the simplest arrangement there are three zones: under the lower limit, accept between the two limits and over the upper limit. Underweight packs are always rejected. Whether overweight packs are rejected is the producer’s decision: a little overfill is no problem for the customer, but a pack far above the upper limit usually points to a fault such as two packs riding together or the wrong product entering the line.
Lines that need closer control use multi-zone classification. For example, a “warning” band is placed just below and just above the accept zone; packs in these bands are not rejected but are counted. When the number of packs falling into a warning band starts to rise, it is clear that filling is drifting before any packs are rejected. In the same way, an alarm or a line stop can be set up after a given number of consecutive underweight packs. Which zones are used and what happens in each is defined product by product.
How are rejected packs removed?
The reject mechanism matters as much as accurate weighing: a pack that is weighed correctly but not removed still reaches the customer. The common methods, and the products they generally suit, are:
- Pusher: A pneumatic or electric ram pushes the pack sideways. Suits flat-bottomed boxes and medium-weight packs; at very high speeds the stroke time of the ram becomes a limit.
- Air-blast rejector: A short burst of air blows a light pack off the belt. Fast and contact-free with pouches, small boxes and light products; not enough for heavy ones.
- Drop flap: A belt section or flap at the outfeed opens downwards and the pack falls into a bin below. Takes little space with pouches and soft packs that can tolerate a drop; not used with glass or fragile products.
- Diverter arm: An arm swings across the line and steers the pack onto a side belt. Gives gentler rejection for heavy boxes, cases and products prone to toppling.
Which method is used is chosen to suit the line and the product. Rejected packs should be collected in a locked bin or on a separate belt, so that faulty product cannot find its way back onto the line. On critical lines, a sensor confirming that the rejected pack actually reached the bin and a bin-full detector are added as well.
Weight rules for prepacked products
The quantity printed on the pack is the nominal quantity, and for prepacked products the way it must be delivered is set by legal metrology rules. The general approach is based on the average quantity principle and contains three basic rules:
- The average content of the packs in a batch must not be less than the nominal quantity.
- The proportion of packs short by more than the tolerable negative error, which is set according to the nominal quantity, is limited to a small percentage.
- No pack may be short by far more than the tolerable negative error.
Products filled under this system may carry the ℮ mark on the pack. The mark shows that the product has been filled in line with the average quantity principle and that the packer assures this through its own checks. The size of the tolerable negative error depends on the nominal quantity; for detailed values and conditions, the regulations currently in force apply.
For the checkweigher, this means the lower limit is set according to the tolerable negative error logic, while the target weight is placed a little above nominal to allow for the filler’s spread. The wider the spread, the higher the target has to sit. Because the checkweigher measures that spread, how far above nominal the target needs to be is decided by data rather than guesswork.
The cost of overfilling and feedback to the filler
Overfilling looks small but builds up because it repeats on every pack. The calculation below is only an example; you can repeat it with your own figures:
- Average overfill per pack: 2 g
- Packs per day: 30,000
- Daily giveaway: 2 g × 30,000 = 60 kg
- Over 300 working days a year: 60 kg × 300 = 18 tonnes
Multiplying those 18 tonnes by the cost per kilogram of your own product gives the annual value of lowering the average by just 2 g. The same reasoning applies to the spread: as the filling spread narrows, the target can move closer to nominal. An improvement that halves the spread allows the target margin to be cut by the same proportion.
Feedback makes this improvement automatic. The checkweigher continuously tracks the average of the latest packs and, when the average moves away from the target, sends a correction signal to the filling machine; on multi-head fillers the correction can also be made head by head. Filling is thus pulled back to target without waiting for the operator. Whether this link can be made depends on whether the filler accepts an external correction signal; we check what your existing machine supports when preparing the quotation.